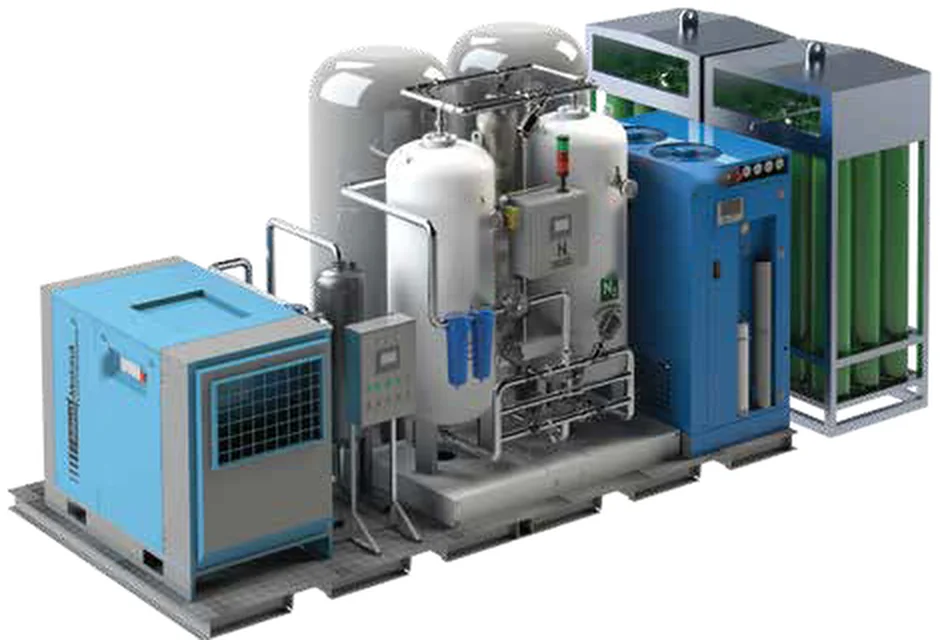
Some projects don't start with a meeting or a quotation. They start with a look: the look of a client who isn't after a catalogue of machines, but wants to know whether the person in front of them really knows what they're talking about. In laser cutting of stainless steel, mistakes can't be swept under the carpet: nitrogen has to be pure, stable and reach the nozzle at 25 bar, no excuses.
This project was exactly that: a test of credibility. And it was passed with calculations, with presence on site and with many hours in the middle of summer.
The challenge
The client was a metal fabricator with three laser cutters, from 3,000 to 7,000 W, working mainly stainless steel: single parts and complete structures, 2 to 20 mm thick, almost three shifts a day, five days a week. They needed nitrogen at 22–25 bar, with stable purity and high flows, and wanted to stop depending on external supply and cut costs from day one.
The starting data were annual consumption figures. A nebula, to borrow an astrophysicist's word. It had to be turned into a plant able to keep all three lasers at full output, with room to grow, because if the client sells more, it will use more nitrogen.
Telling the truth, even when it's uncomfortable
At the presentation I told the client how things stood: it would be a demanding installation, summer would add obstacles (heat, dust, a harsh industrial environment), but the plant would work and the savings would start from day one.
Explaining the truth with technical clarity sometimes meets resistance. But I believe keeping quiet is far riskier than causing discomfort, because in engineering whatever is hidden usually ends up reappearing as a problem. The client listened, looked me in the eye and trusted me. That changed everything.
Why summer matters
A PSA plant is not a black box. It is a living system, where every variable depends on the others:
- Cycle time and the retention capacity of the carbon molecular sieve.
- Mass transfer coefficients.
- Pressure balance and regeneration dynamics.
- The real temperature in the bed and losses from physical adsorption.
- The balance between flow, purity and pressure, in real time.
In the heat, all of this works against you. Air arrives hotter and wetter, the dryer runs at its limit, the compressor delivers less and the sieve retains less oxygen per cycle. That is why a plant for a fabrication shop is sized for August conditions, not catalogue conditions. And that is why purge losses must be optimised and instantaneous flow adjusted so that purity doesn't move when all three lasers demand at once.
The high-pressure chain
A laser doesn't consume continuously: it draws a lot of flow while cutting and almost nothing between parts. The answer is to separate production from consumption. The PSA generator produces steadily, a booster raises the nitrogen to 300 bar and stores it in cylinder bundles, and from there it is regulated to cutting pressure. The bundles act as a buffer: they absorb the lasers' peaks and the generator works calmly.
Working at 300 bar is no joke. Not everyone has the knowledge, the skill or the sense of responsibility to install and operate at those pressures. The installation team rose to the challenge: rigorous, proactive and professional. Without their work, the project would not have progressed as solidly as it did.
When theory puts on its overalls
For weeks I was alongside the client. Not just designing: at commissioning, in quality control, verifying nitrogen purity, supporting the installers and adjusting parameters. Maths, physics and sweat.
I remember one summer evening. I was driving back from Monzón after working on a heat-regenerated adsorption dryer; one of those long days, early start included. Before going home I stopped at the plant: I wanted to see with my own eyes that the cylinder bundles were full and the nitrogen quality was right, so they could cut the next day without surprises.
The client never asked me for an electrical diagram or a P&ID. He never asked about the PSA cycle or the valves. He looked me in the eye. And that says a lot.
What catalogues don't tell you
Trust can't be given or forced: it is built. And it isn't built with marketing or catchphrases, but with presence, consistency, applied knowledge and hours. Some people only look at the equipment; others look you in the eye. Those are the clients worth working with, because they're not just after nitrogen: they want honest solutions that don't fall apart when the summer fan blows harder than expected.
In the end, nitrogen isn't sold. It's proven.
And no, I won't put the diagrams, the pressures or the tricks for optimising the cycle without losing purity here. Explain everything and people call you to copy it… or to ask you for a job. I'll keep an ace up my sleeve, at least until the heat eases off.