GAS4U — Data intelligence for energy management of industrial gases
Hardly any plant knows what each Nm³ of gas really costs. The flowmeters, analysers and electricity meters are already there, but their data are never combined or even looked at. GAS4U brings them together, tells you what is going on and, with AI, what is about to happen.
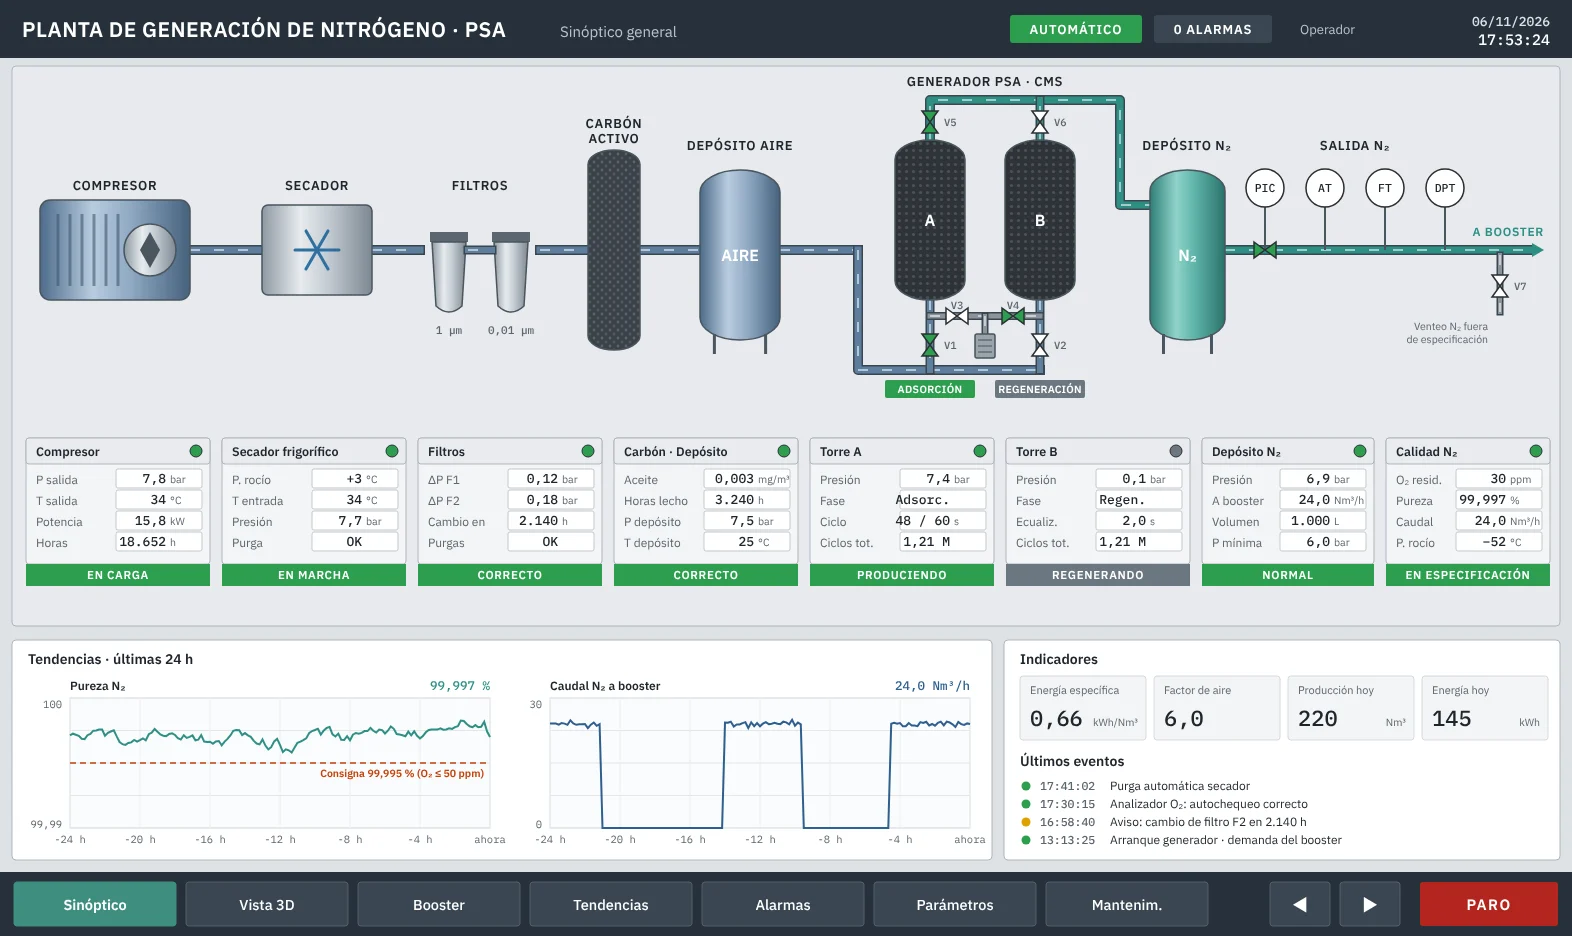
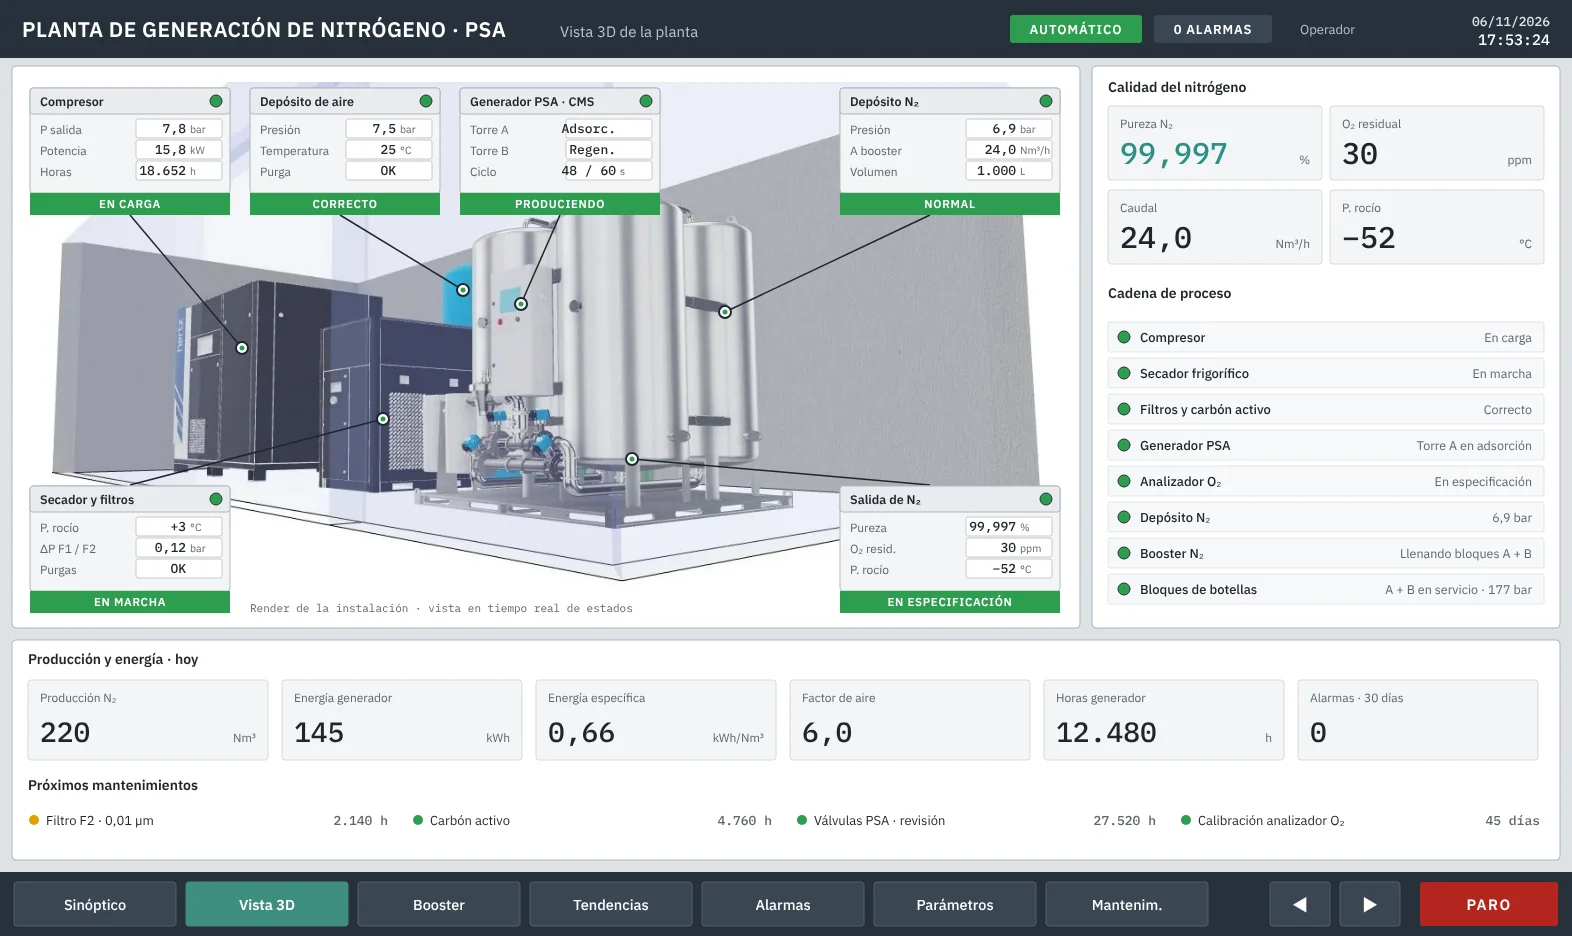
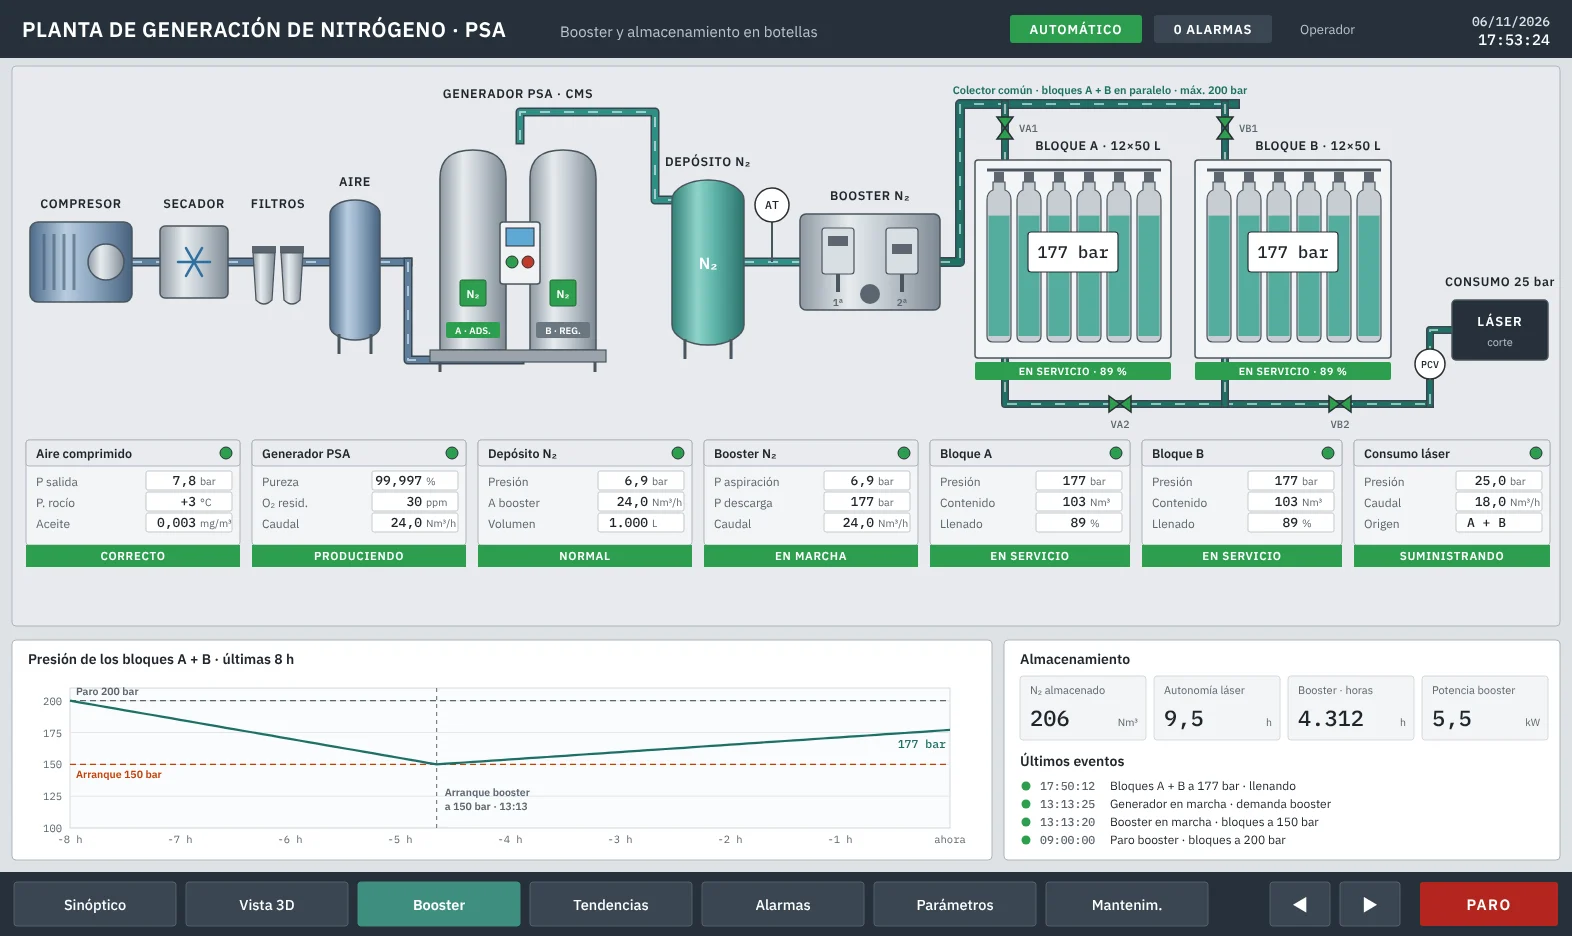
A 99.997 % nitrogen plant for laser cutting. In Synoptic and 3D view you see the generation side: compressor, dryer, filters, activated carbon, PSA generator and N₂ buffer. In Booster you see the high-pressure side, with the booster and two cylinder bundles at 200 bar. Values change every second; press STOP to stop the plant.
Simulation with sample data. Compatible with Modbus, OPC-UA and MQTT · SCADA integration · standalone or integrated operation. Open full screen →
GAS4U screens
Every piece of equipment in the plant, in a single view
Your plant's data already exist: pressures, flow, residual oxygen and production totals appear every second on each unit's screen. But nobody stores them or cross-checks them against the electricity bill. GAS4U brings them together in a single view, stores them and alerts you when something drifts.
Synoptic · compressed air, PSA and N₂ quality3D view · status of each unit in the generation roomBooster and cylinder bundles at 200 bar
Intelligence · AI
What the AI in GAS4U does
The AI in GAS4U is no magic and doesn't replace your judgement. It works on the sensors your plant already has and does three things nobody can do while watching several plants at once: combine, anticipate and alert.
01 · COMBINE
Joins what nobody cross-checks
It gathers flow, N₂ purity, residual O₂, pressures, dew point and electricity consumption —readings that are already there but that nobody compares— and works out what really matters: the true cost of each Nm³, the air factor and the generator's performance. The payback, which shows up on no invoice, finally becomes visible.
02 · ANTICIPATE
Warns before it becomes a failure
It learns each plant's normal behaviour and spots the deviation in time: a filter whose differential pressure starts to climb, a sensor drifting from the reference, a consumption that spikes. It projects the trend and tells you when to act. Predictive maintenance, not reactive.
03 · ALERT
Tells you in plain language
It turns everything into something you can act on: which plant needs attention this week, where money is being lost and which certificate is due soon. No dashboards nobody looks at: the conclusion, when it's needed, and without standing in front of the unit.
N₂ quality is still measured on site, with calibrated equipment. The AI does not replace it: it keeps watch the rest of the time, when nobody is there.
Plant connection
How we connect your equipment to GAS4U
We use the PLC and screen your generator, compressor or dryer already has. We add an industrial router that opens an outbound encrypted tunnel: no port is opened on your network and your IT department does not have to do anything. Choose your PLC brand and connection type to see how it looks.
PLC brand
Internet connection
Already installed in the equipmentWhat we addIndustrial EthernetOutbound encrypted VPN tunnelData to GAS4U
Swipe the diagram sideways to see all of it →
Tap any element of the diagram
Industrial router · what we add
It is the only new device in the cabinet. It mounts on DIN rail, is powered at 24 V from the existing supply and connects with one cable to a free switch port. It opens an outbound encrypted tunnel and reads the PLC data.
What we add to the cabinet
Industrial router with VPN and PLC reading, on DIN rail.
4G/5G modem with data SIM and external antenna (or connection through the customer network).
Fuse terminal and 24 V wiring from the existing supply.
Network cable to a free port on the equipment switch.
Installed in a few hours, with the equipment running or during a short stop.
Compatibility
PLC
Software
Data reading
Siemens
TIA Portal · STEP 7
S7, OPC UA
Omron
Sysmac Studio · CX-One
EtherNet/IP, FINS, OPC UA
Unitronics
VisiLogic · UniLogic
Modbus TCP, PCOM
Schneider
EcoStruxure Machine Expert
Modbus TCP
Others
Manufacturer's
Modbus TCP, OPC UA
If the equipment only has Modbus RTU (RS-485), we add an Ethernet gateway.
Security
No open ports: the connection always goes outbound from the equipment.
End-to-end encrypted tunnel.
User-based access, only to authorised equipment, with a connection log.
Machine network separated from the customer's office network.
Remote access can be disabled from the plant itself.